How we work
One accountable partner, many specialist factories
We are a trading company, not a manufacturer. Our job is to match each construction to the right factory — then make sure the work is done properly, on time, and to your spec.
Our model
What a trading partner actually adds
A leather motorcycle boot and a knit running shoe are rarely made on the same line. Choosing who makes what — and holding them to it — is the whole job.
Match
We choose the factory by construction and material, from partners we have worked with for years — not by whoever quotes lowest this month.
Control
Sampling and approval first, then in-line checks, lab testing and final inspection. Nothing ships on trust alone.
Deliver
Consolidation, export documentation and logistics handled from Hong Kong — one contact, one schedule, one invoice.
Development flow
From tech pack to mass production
The path every style follows — from your drawings to a running production line.
Receive tech pack & match factory
Evaluate the tech pack and match a suitable partner factory.
Trial pattern by our technicians
Trial pattern run by our technicians to confirm producibility.
Material sourcing to target price
Match raw-material suppliers to the client's target price.
Develop pattern & T1 sample
Cut the pattern from the design and build the T1 prototype.
Wear-test, feedback & iterate
Client wear-test feedback drives the T2…Tn iterative loop.
Approved → mass production
Client approval closes development and transfers to mass production.
Pre-production validation
Third-party test before production
Before bulk cutting starts, materials and components are sent to accredited third-party laboratories. Tests are scoped to your destination market's regulations and the agreed quality standard — we do not release an order to production until the report comes back clean.
Abrasion test
Outsole and upper materials are rubbed under fixed load and cycles to confirm the wear rate meets the target spec before bulk cutting starts.
Yellowing resistance test
White and light-coloured materials are exposed to UV and heat to verify they will not yellow within the agreed shelf life.
Waterproof & breathable bootie test
The highly breathable waterproof sock liner is submerged and flexed under water to confirm zero penetration, while moisture-permeability testing keeps the breathability of the bootie within the agreed spec — dry outside, comfortable inside.
Flexing test
Finished soles and complete shoes are flexed through 100,000 cycles at the forefoot crease line to confirm the outsole and bonding survive repeated bending without cracking.
Additional tests — elasticity, slip resistance, colour fastness, formaldehyde, heavy metals, PFAS, REACH and Prop 65 — are arranged per destination market.
Production stages
The seven stages we supervise on every order
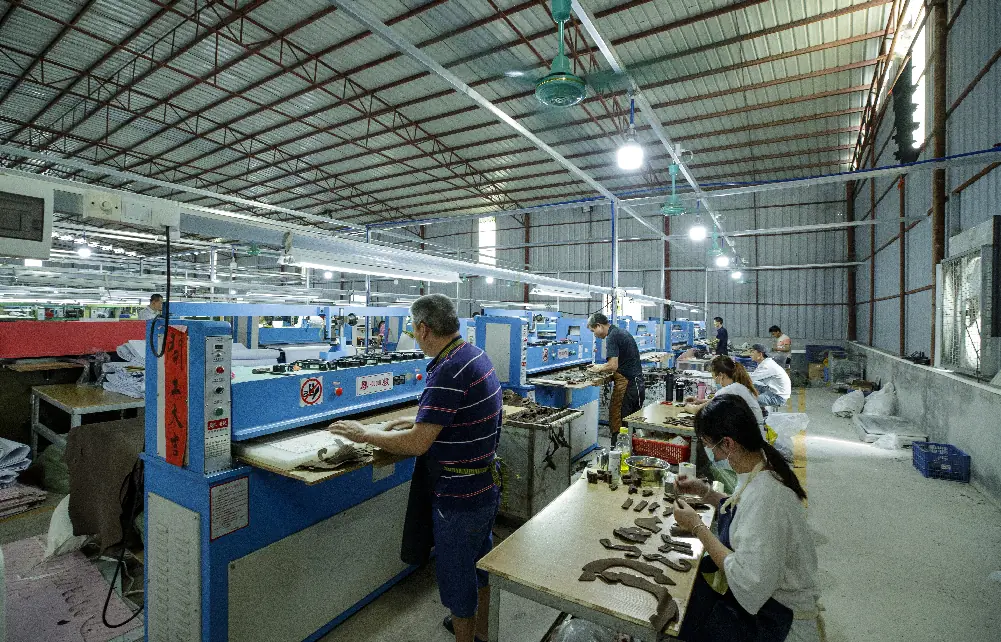
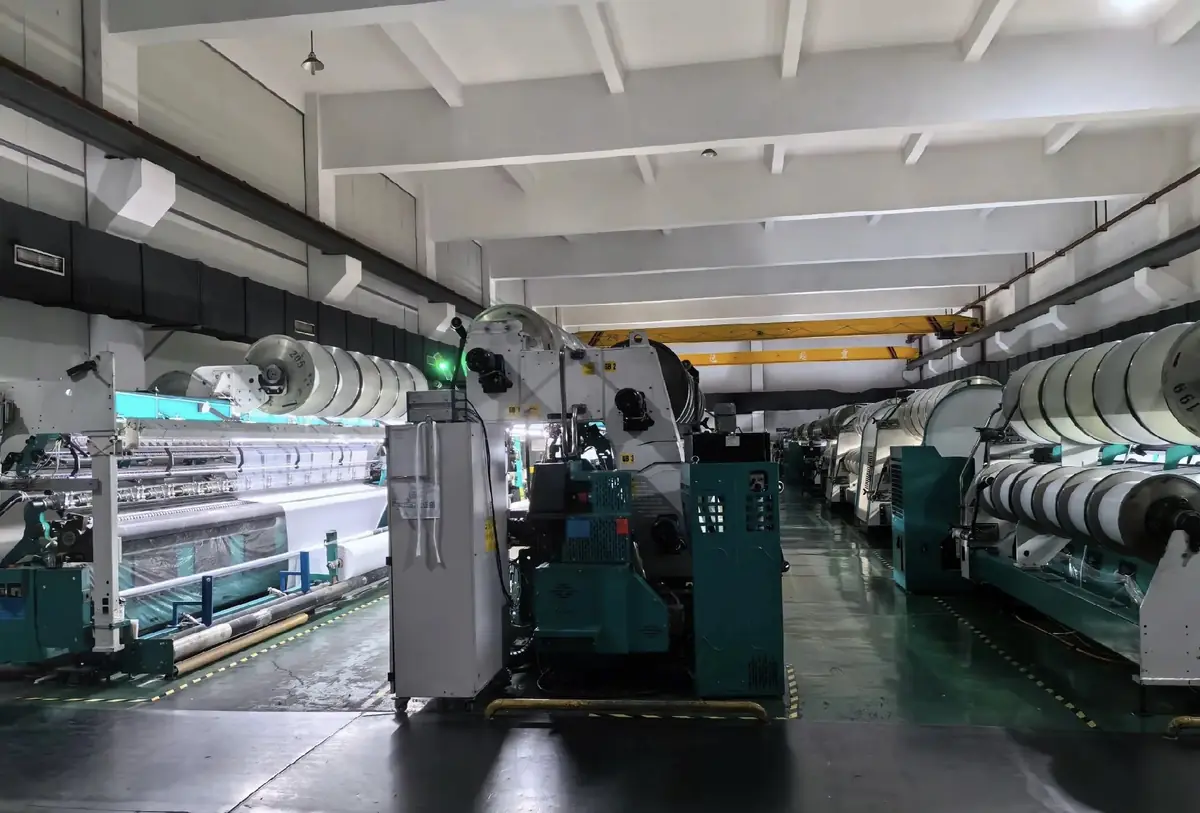
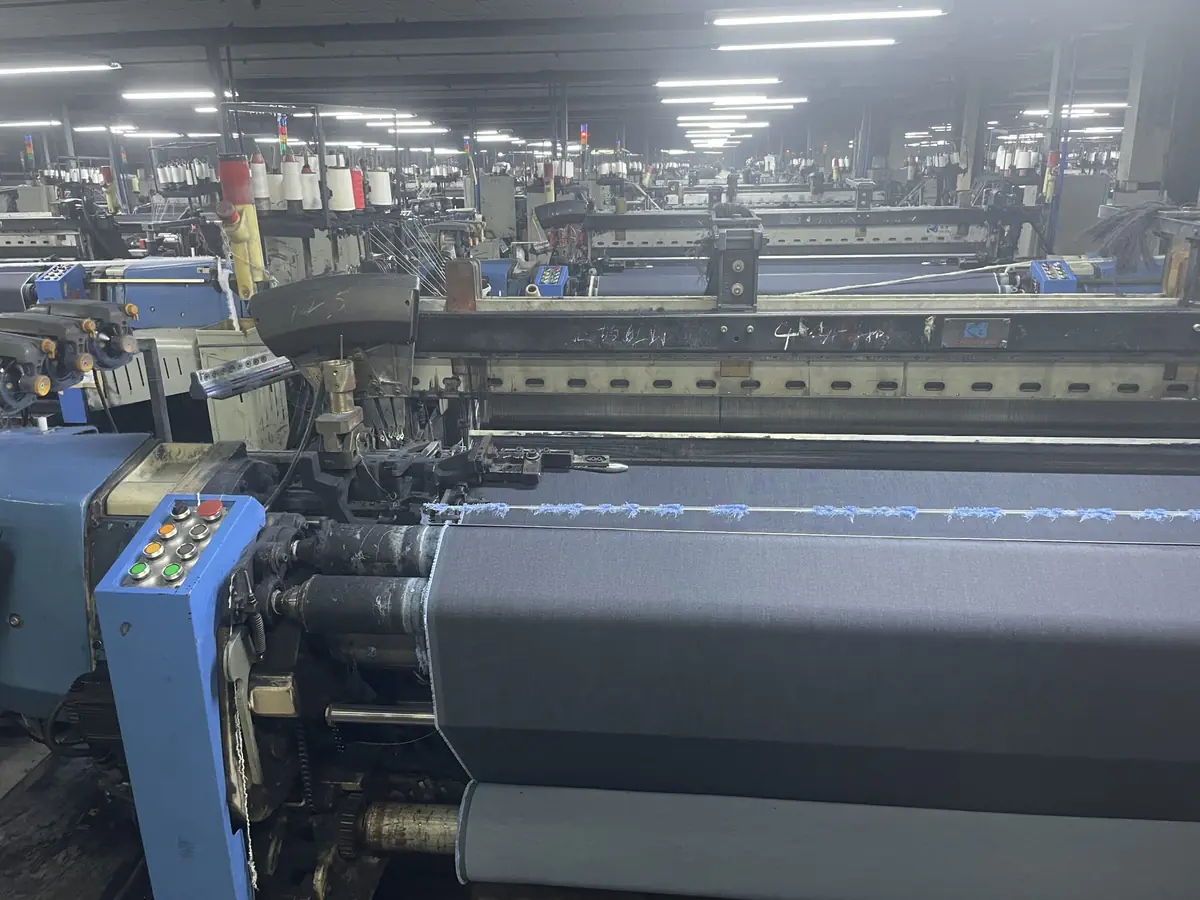
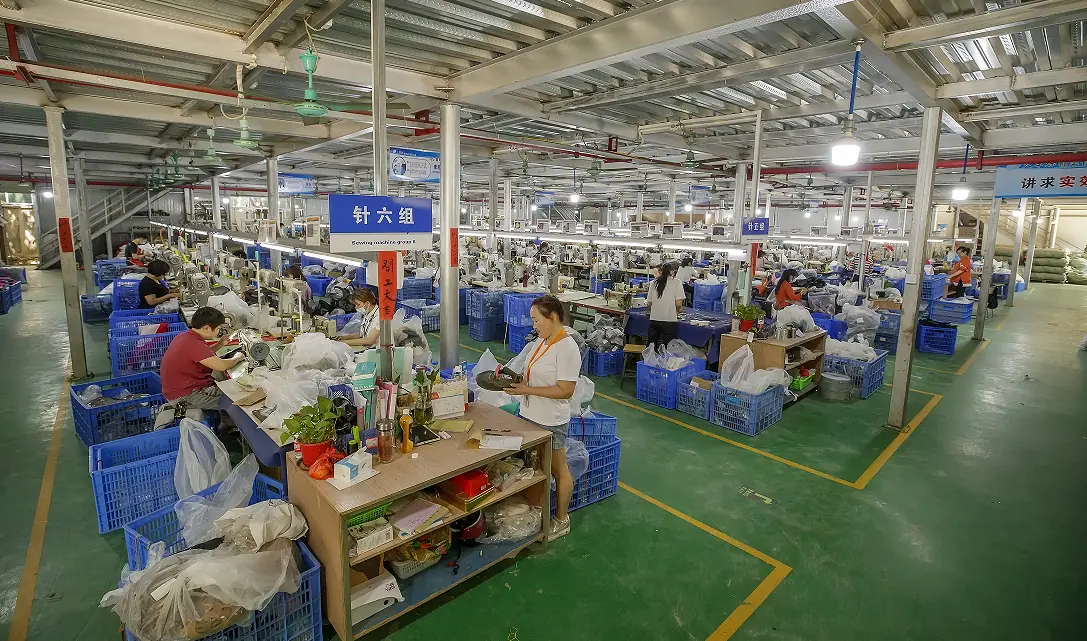
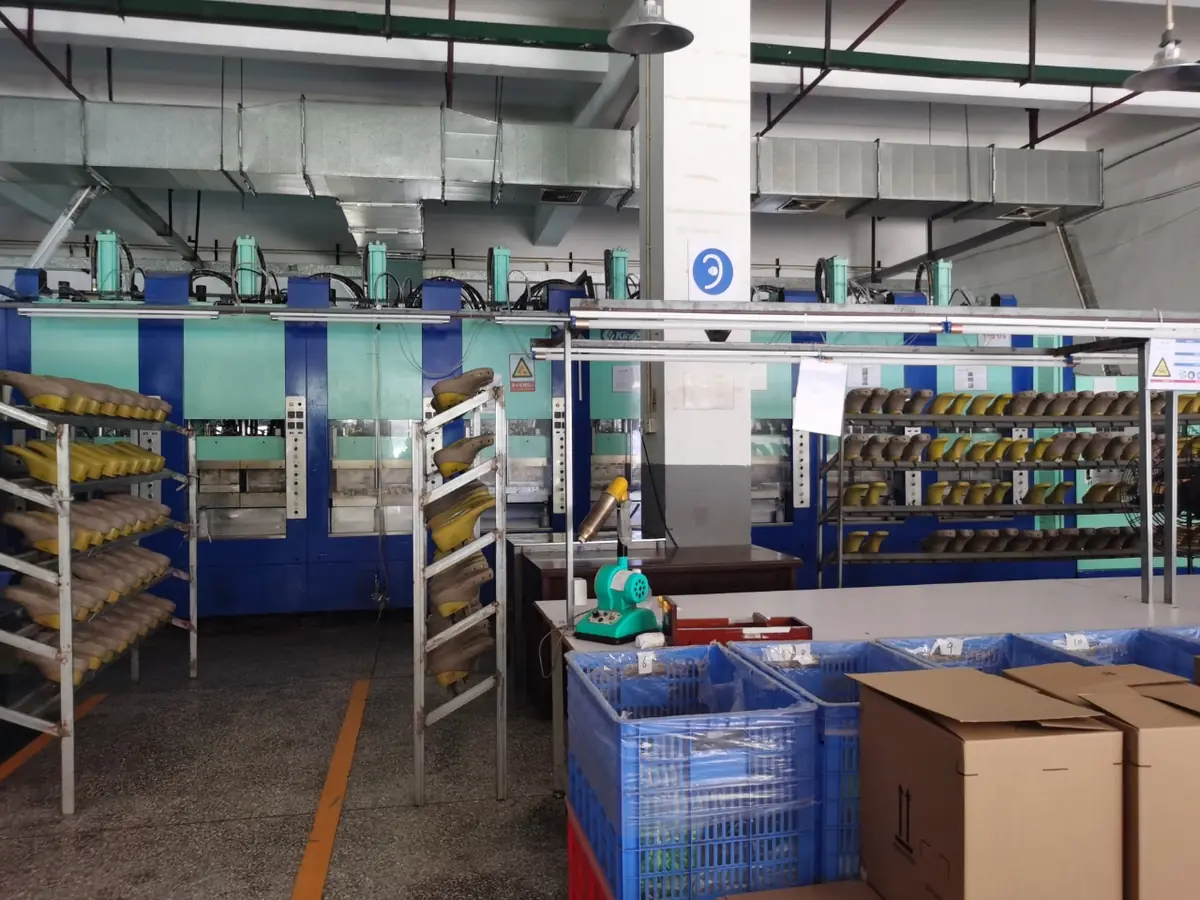
Photographs show production lines at our partner factories.
Cutting & material preparation
Before the line starts, we approve materials and the cutting plan: parts, sizes and quantities against your drawings, material inspection for defects and colour variation, and layout with templates or CAD to keep utilization sensible.
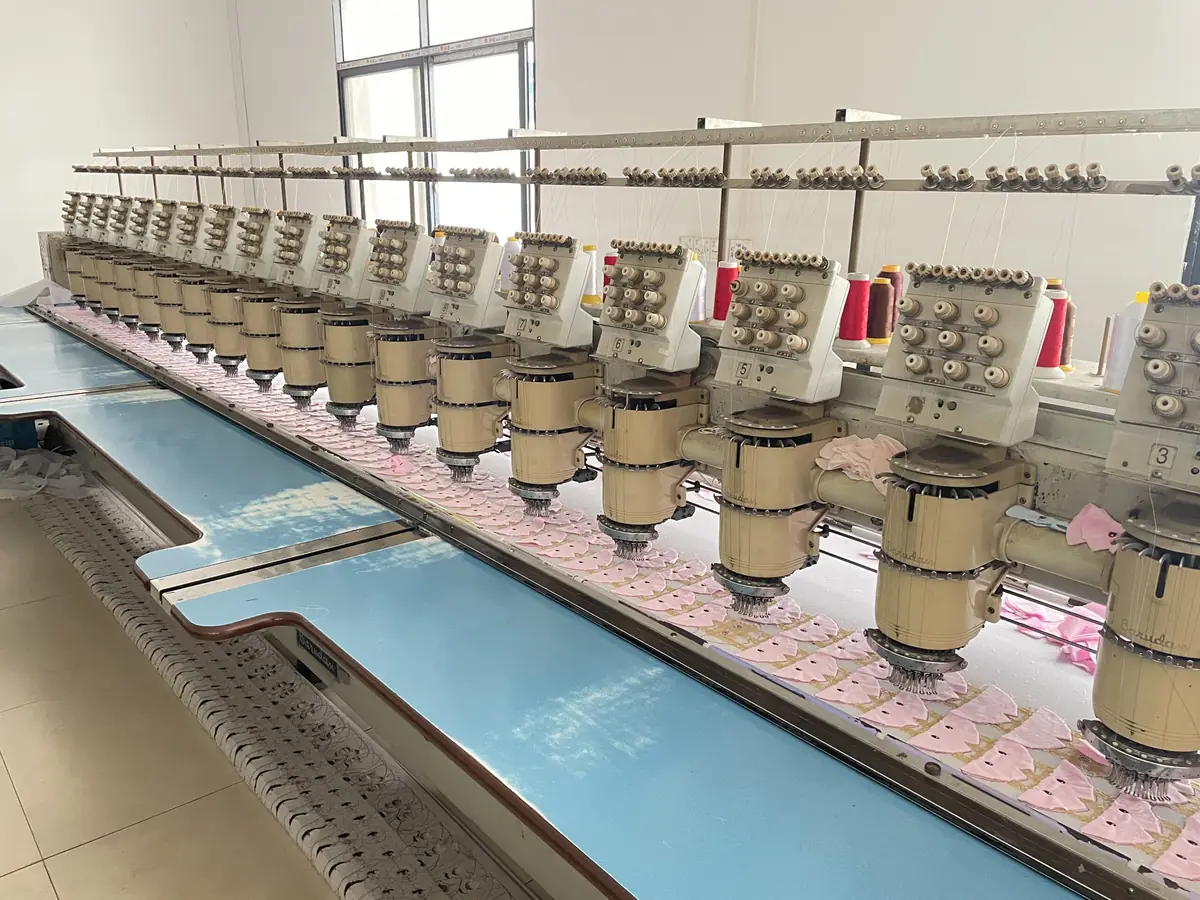
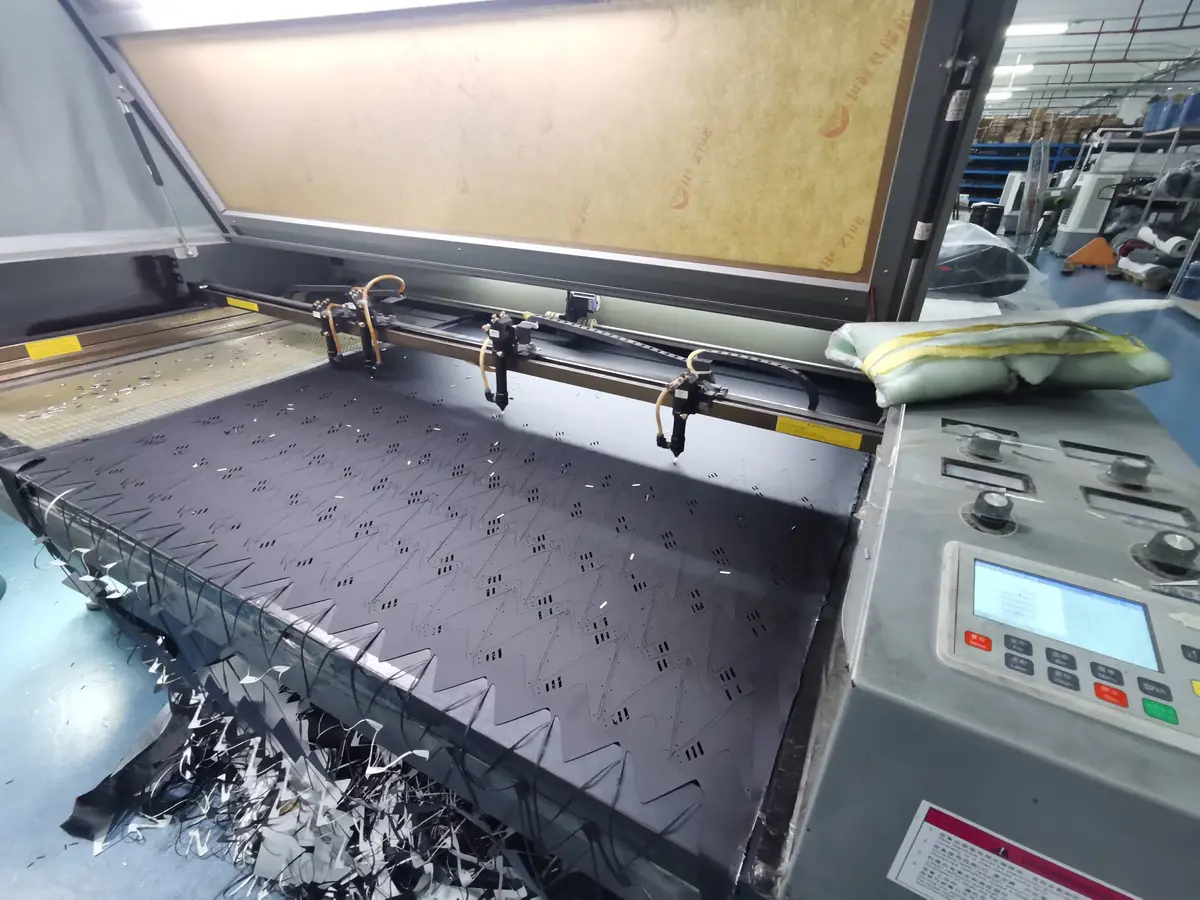
Embroidery & laser decoration
Logos and patterns run on multi-head embroidery machines with controlled stitch density and thread colour; laser engraving creates fine textures and perforations. Both are handled by specialist partners we supervise, so decoration stays consistent across the run.
Warp-knit & fabric uppers
Engineered uppers are knitted from polyester, polyamide and spandex-core yarns on warp-knit machines following CAD patterns, then dyed and finished for colour and durability before cutting and stitching.
Sewing & lasting
Cut components are stitched into complete uppers, then lasted over the form to lock in shape and fit. This is where a design stops being a drawing — and where we check fit against the approved sample.
Outsole assembly
Outsoles are roughed, primed and glued, then pressed with calibrated pressure and timing to bond midsole and outsole. Bond strength and alignment are checked before the pair moves down the line.
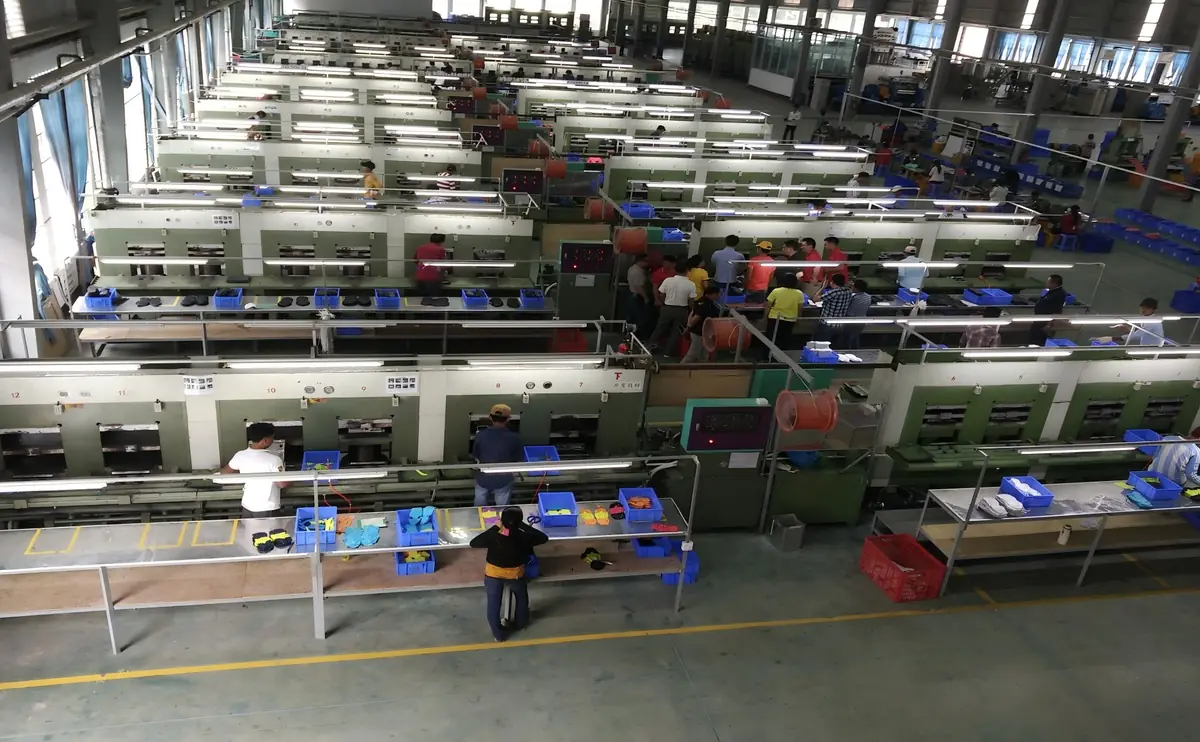
Inspection & packing
Finished pairs are inspected for bonding, appearance, sizing and comfort, with material and durability testing through partner laboratories. Approved pairs are cleaned, packed and cartoned to your packing specification.

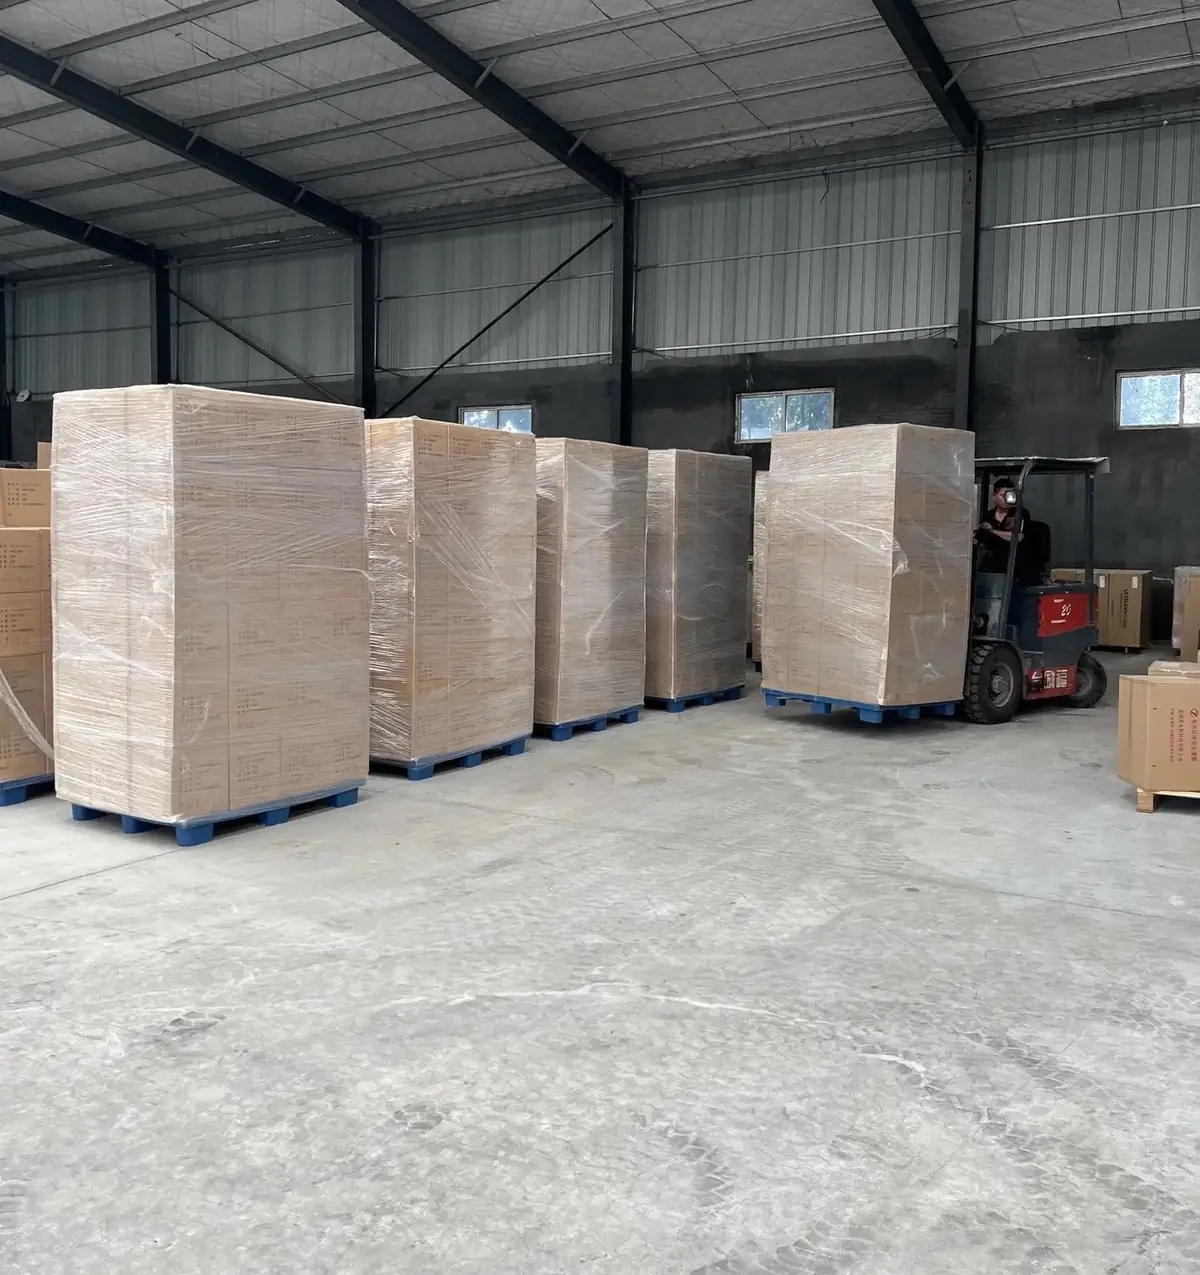
Warehouse & export logistics
Finished goods are consolidated and dispatched on schedule. Export documentation, freight booking and shipping coordination are handled by our team.
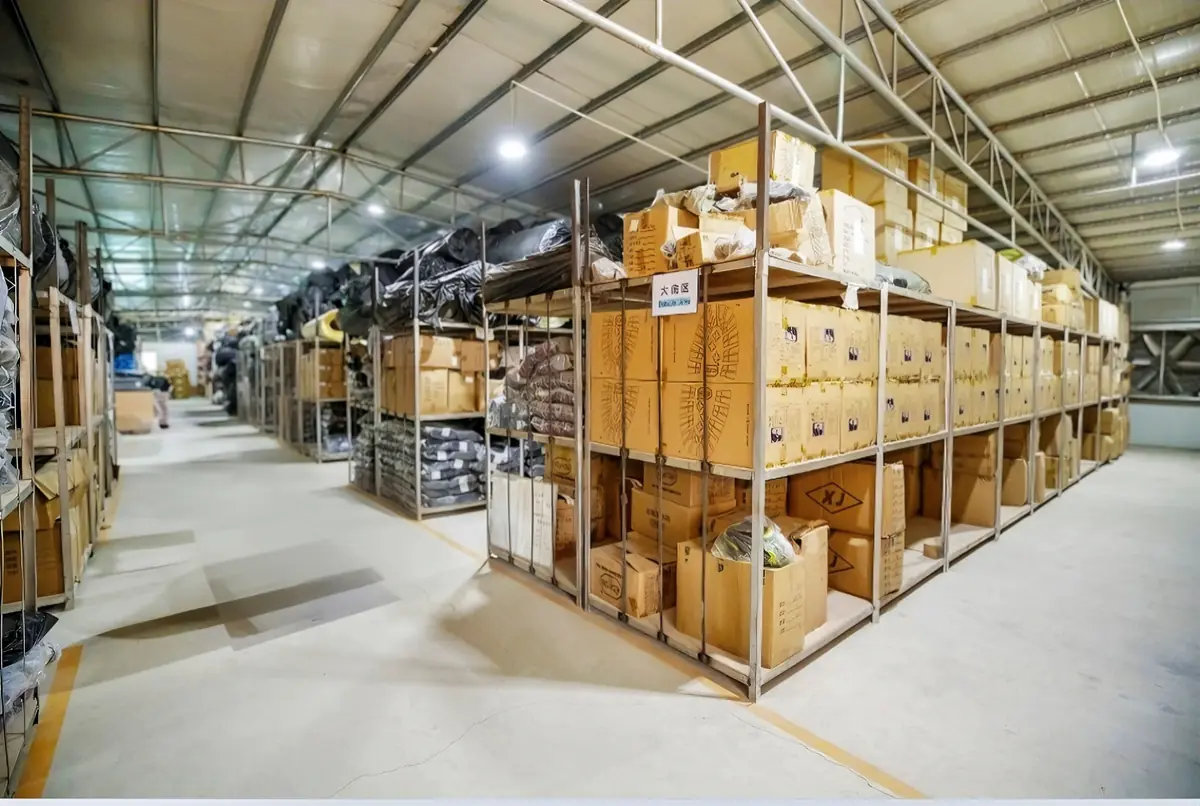
Quality gates
Where we stop the line
Four checkpoints, defined before production starts and reported to you in writing.
| Gate | What we check | Outcome |
|---|---|---|
| Pre-production | Materials, components, colour approval, cutting plan, approved sample on site | Bulk release — or hold |
| In-line | Stitching, lasting, bonding, measurements against the approved sample | Rework before it spreads |
| Pre-packing | Appearance, sizing, pair matching, labelling and packing spec | Sort-out and correction |
| Pre-shipment | Carton count, shipping marks, documentation | Release for export |
Want to see the factories?
Ask us to arrange a visit — sample room and production lines included.